Surface finishing is where a lot of machined parts gain their final cost, and where specification is often thinnest on the drawing.
Anodising — aluminium only
An electrochemical conversion of the surface into aluminium oxide. It grows into and out of the surface, so it changes dimensions slightly.
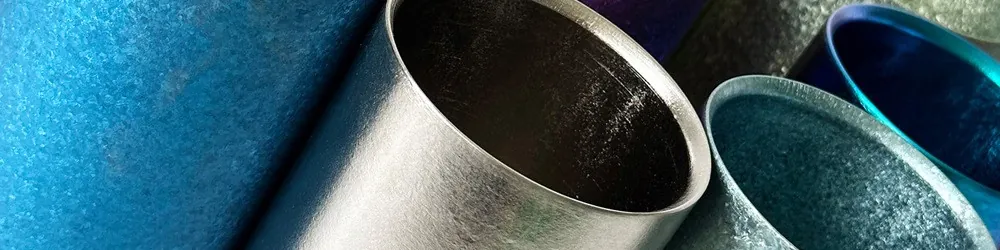
Type II is the common decorative and mild-protection option, available in colours. Type III (hard anodise) is thicker, much harder, and used for wear surfaces — but it builds more dimension and is usually natural or dark in colour only.
What to specify: type, class, colour, and which surfaces are masked. Threads and precision bores are often masked, and if you do not say so, the finish goes on them and the dimension moves.
Passivation — stainless steel
Not a coating. A chemical treatment that removes free iron from the surface and lets the natural chromium oxide layer reform evenly. Adds essentially no dimension.
Used on stainless parts, particularly medical and food contact, where surface iron would cause rust spots.
What to specify: the standard being worked to, and whether a test is required on the batch.
Plating — most metals
A deposited metal layer: zinc, nickel, chrome, tin and others. Adds dimension, and unlike anodising it sits entirely on top of the surface.
Zinc is the low-cost corrosion option for steel. Nickel gives hardness and a bright finish. Tin is used for electrical contact surfaces.
What to specify: metal, thickness, and any post-treatment such as passivate or seal.
The four questions that decide
Base material? Anodising is aluminium only. Passivation is stainless only. Plating is broad.
Does the dimension matter? Anodise and plating both build. On a close-fitting bore or a thread, this must be accounted for in the machined size — which means the supplier needs to know the finish before machining, not after.
Is it cosmetic? Then colour consistency across batches becomes a specification in itself, and the machined finish underneath matters as much as the coating.
What environment? Indoor electronics, outdoor exposure and salt spray are three different requirements. If corrosion performance is critical, specify a salt spray hour requirement rather than naming a finish and hoping.
The most common mistake
Sending a drawing with a finish note and no masking information. The result is coated threads that no longer accept the fastener, or coated bores that are now undersize. Mark clearly which features are masked, or state the dimension as "after finish" so the machinist can adjust.
The short version
Match the finish to the base material first, then decide whether dimensions or appearance drives the specification. And always say what is masked — it is the single most common omission on finishing callouts.